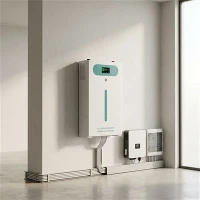
Hebei Mutian Solar Energy Technology Development Co., Ltd. is one of the most reliable manufacturers and suppliers of 51.2v400ah lifepo4 battery in China, also supports customized service. Welcome to buy advanced 51.2v400ah lifepo4 battery in stock from our factory.
Key Visual Highlights
To give you a clearer understanding of our 51.2V400AH LiFePO4 Battery, we have highlighted the core features and design details below.

High-capacity battery core
The high-capacity battery core utilizes the 400AH Lithium Iron Phosphate cells in a compact design with a high energy density and an excellent ability to dissipate heat.

Intelligent touchscreen display
The built-in touchscreen enables real-time monitoring of battery parameters like voltage, current, temperature, and remaining capacity.

Rich communication port
The battery is equipped with RS232, RS485, and CAN communication ports, which makes it fully compatible with many of the available inverters and monitoring systems.

Rugged metal enclosure
The tough metal casing helps protect the battery from any mechanical damages or any environmental effects, which will ensure reliable operation in a long time.

Built-in BMS protection module
The innovative battery management system continuously monitors and balances cells voltage, thus preventing overcharging, over-discharging, excess current, short circuiting, and overheating.

Bluetooth and Wi-Fi
The innovative built-in module enables wireless monitoring through its dedicated application.
Product Features & Operational Notes
Key Advantages
Superior Safety and Stability – LiFePO4 chemistry provides exceptional thermal and chemical stability, significantly reducing the risk of thermal runaway compared to other lithium chemistries. This makes it one of the safest battery options for residential and commercial applications.
Exceptional Cycle Life – With 8,000 life cycles, this battery offers years of reliable daily use, far surpassing traditional lead-acid or NMC batteries. This translates to a lower total cost of ownership over the system's lifespan.
Intelligent Self-Management – The integrated BMS performs real-time monitoring of every cell, ensuring balanced charging and discharging. It also automatically protects against abnormal conditions, extending battery life and maintaining performance consistency.
Smart Connectivity – The built-in Bluetooth and WiFi APP modules allow you to remotely monitor battery status, view historical data, and receive alerts, making energy management simple and efficient.
Wide Operating Range – Capable of functioning in temperatures from -20°C to 60°C and at altitudes up to 4000m, this battery adapts to diverse environments, from cold mountain regions to hot tropical areas.
Important Usage Notes
Connection: The wires and terminals should be selected properly according to the current rating. All joints must be firmly tightened to avoid loose contacts that may result in overheating.
Charging: Observe the required charge cutoff voltage of 58.4V. The use of incorrect chargers may spoil the battery and cancel the warranty. For solar charging, it is recommended to use solar arrays with a total output of over 400W to ensure adequate charging especially in places with short time of daylight hours.
Storage: If the battery needs to be put in storage for a long stay, charge it 50% – 70% of capacity and keep it in a dry and cool place. Recharge it every 3 – 6 months to keep the battery healthy.
Maintenance: The battery requires minimal routine maintenance. Periodically check the terminals for oxidation and ensure the ventilation openings are not obstructed.
Application Fields
This 51.2V400AH LiFePO4 Battery is designed to meet the needs of a wide range of applications, ensuring uninterrupted power and energy efficiency:
Solar/Wind Energy Storage Systems – Store excess energy generated from renewable sources for use during nighttime or peak demand periods, maximizing self-consumption and reducing grid dependence.
Communication Equipment – Provide reliable backup power for telecom base stations, signal towers, and data communication hubs where stable operation is critical.
Uninterrupted Power Systems - Provide enough power backup to servers, workstations, and networking equipment to keep the data from being lost.
Medical Equipment - Provide clean energy to life-saving appliances and diagnostic machines that must not stop working even for a minute.
Fire and Security System – Provide power to safety systems like surveillance cameras, fire alarms, and intrusion detection systems all the time even during the loss of power.
Company Strength & Certifications
Professional Manufacturing Capabilities
The main field of operation of our organization is to do research and manufacture high-performance lithium battery systems. Owing to years of experience, we use the combination of the newest technologies of manufacturing with the strictest methods of quality control that allow us to make battery systems according to international standards.
Key Strengths:
State-of-the-art automated production lines and precision testing equipment.
A dedicated R&D team with deep expertise in BMS technology and battery pack design.
Strict quality management system covering raw material procurement, production processes, and finished product inspection.
Certifications:
ISO 9001:2015 Quality Management System
ISO 14001 Environmental Management System
CE, RoHS, UN38.3, and MSDS certifications (as applicable)
Production Workshop (Images available upon request):
Automated cell sorting and matching station
Laser welding and module assembly line
Comprehensive BMS testing and battery performance testing area
Hot Tags: 51.2v400ah lifepo4 battery, China 51.2v400ah lifepo4 battery manufacturers, suppliers, factory, high capacity lithium battery, lithium battery budget friendly, lithium battery durability, lithium battery exchange, lithium battery optimizations, lithium battery upgrades